Coating inspection
Independent third-party inspection, from surface preparation to the final film.
Find out more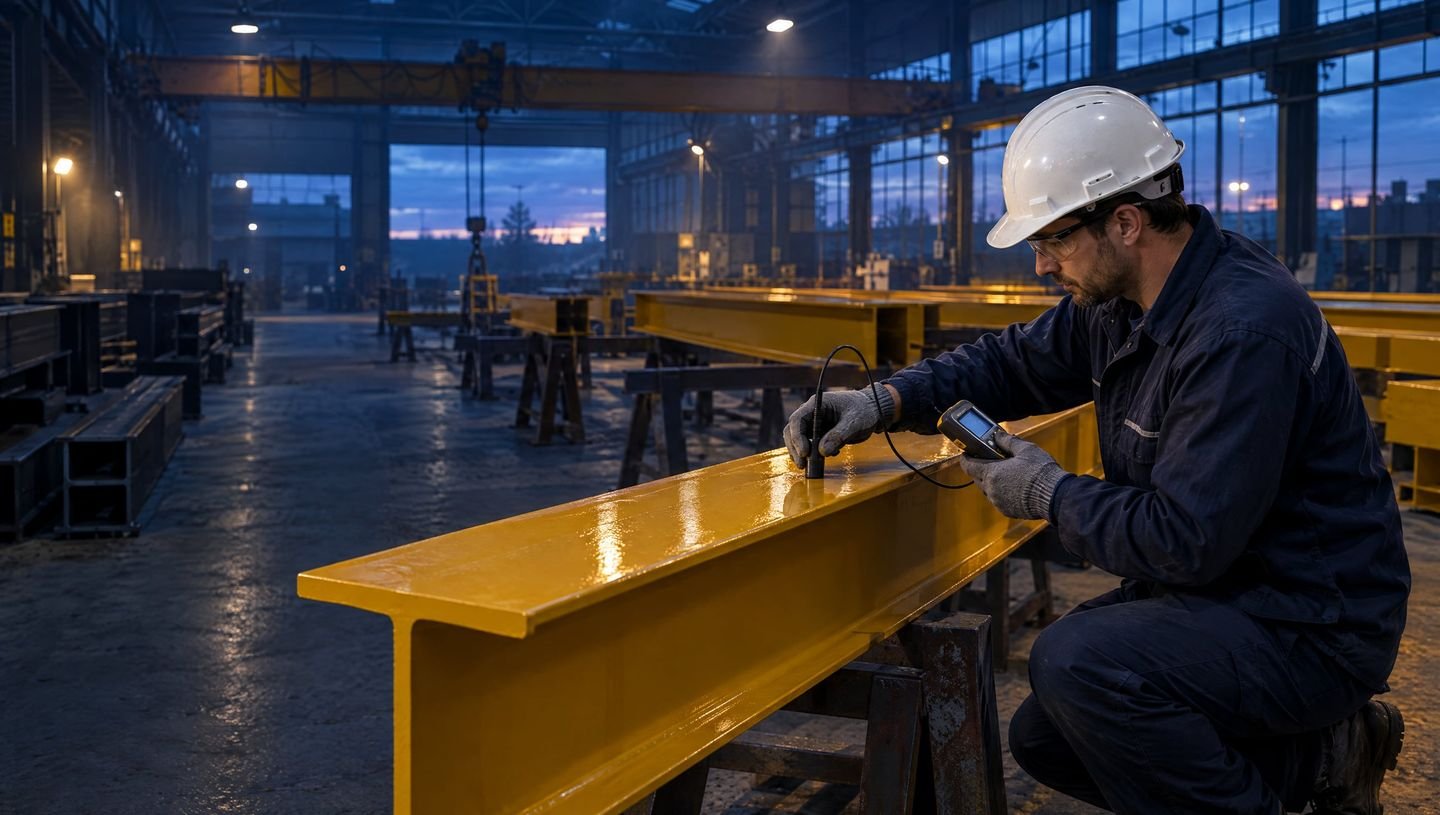
Suffolk · East Anglia · UK
Supporting protective coating projects across the UK, from surface preparation to final sign-off, with a strong presence throughout Suffolk and East Anglia.
Evidence, not opinion
Once a coat is on, the one beneath it can never be checked again. So we measure at every hold point and hand you traceable records your client can rely on.
From the spray booth to sign-off
Most inspectors learn coatings from the outside. We learned them on the line: surface preparation, wet spray, powder coating and metal spraying, then quality management for multi-process finishers.
That is why we know where problems really start, usually well before the paint, and how to stop them before they cost you a rejected delivery or a failed coating.
Most coating failures are decided before the first coat goes on.
What we do
From the specification to the final signature, we cover every stage where a coating can go right or wrong.
Independent third-party inspection, from surface preparation to the final film.
Find out more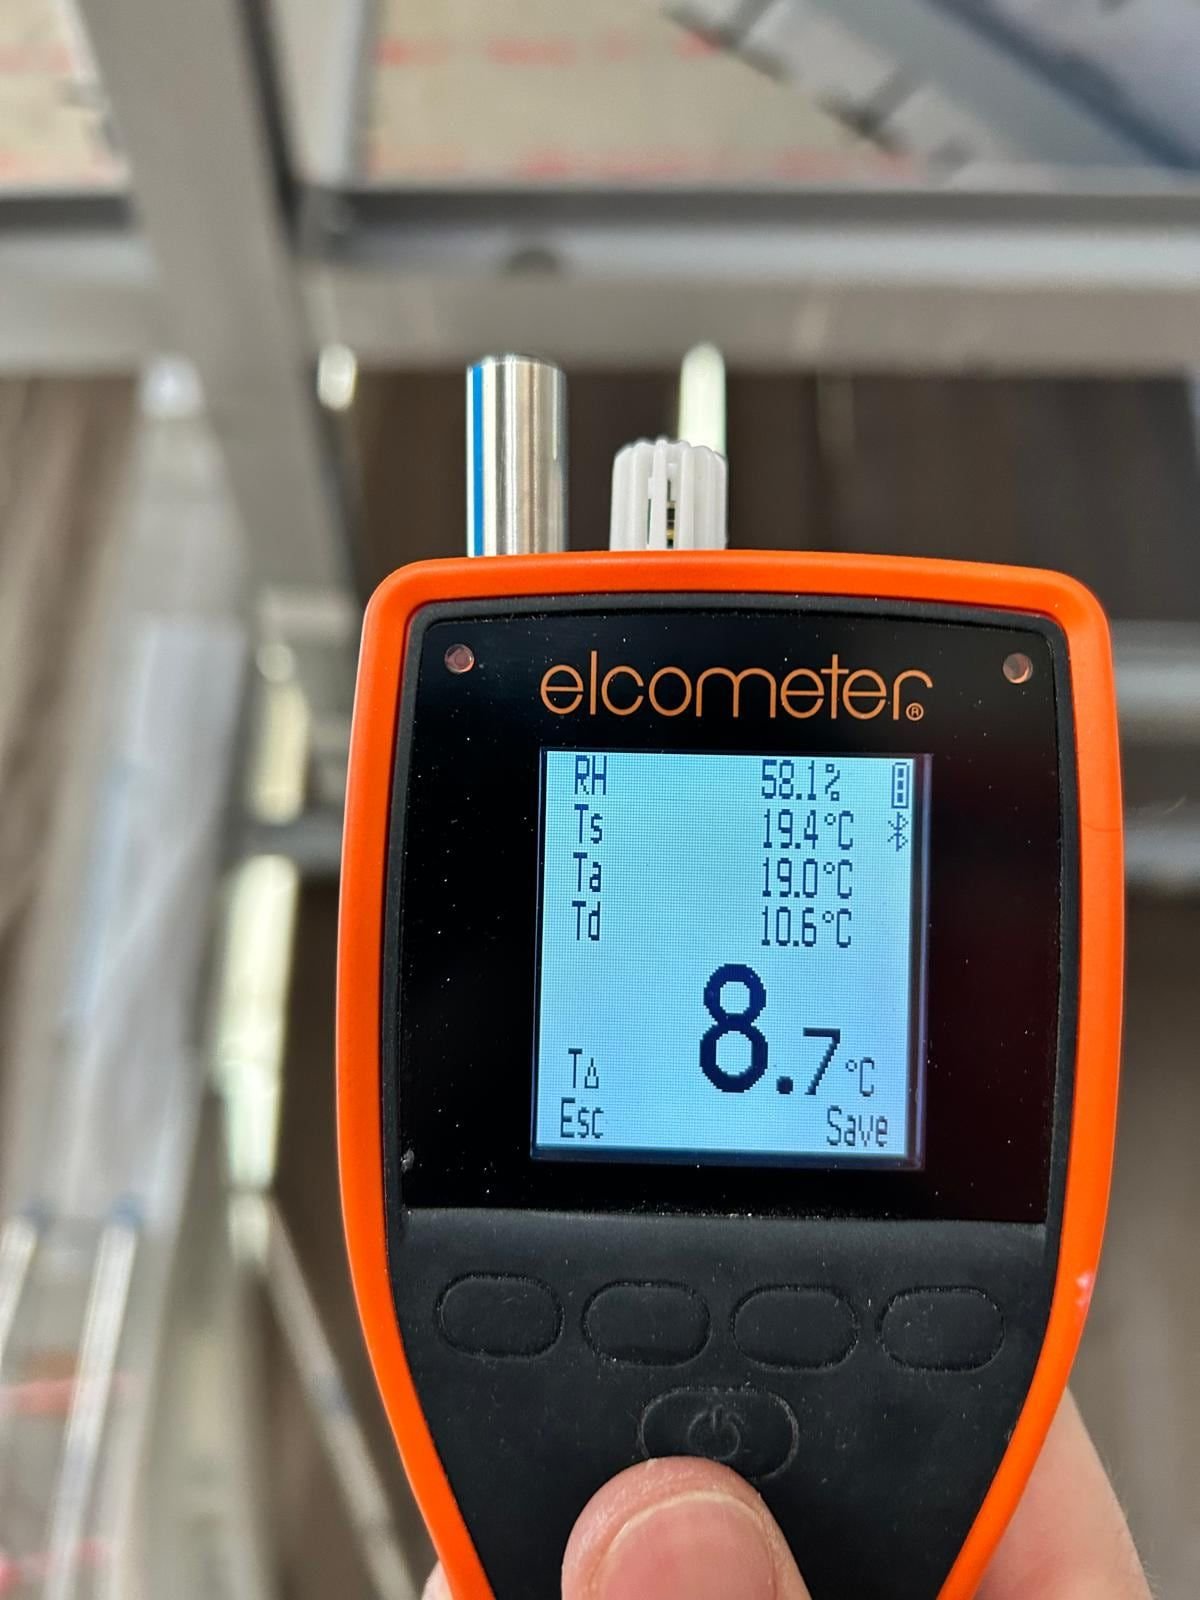
Inspection and test plans, QC systems and documentation your clients will trust.
Find out more
Coating specifications and system selection matched to environment, life and budget.
Find out more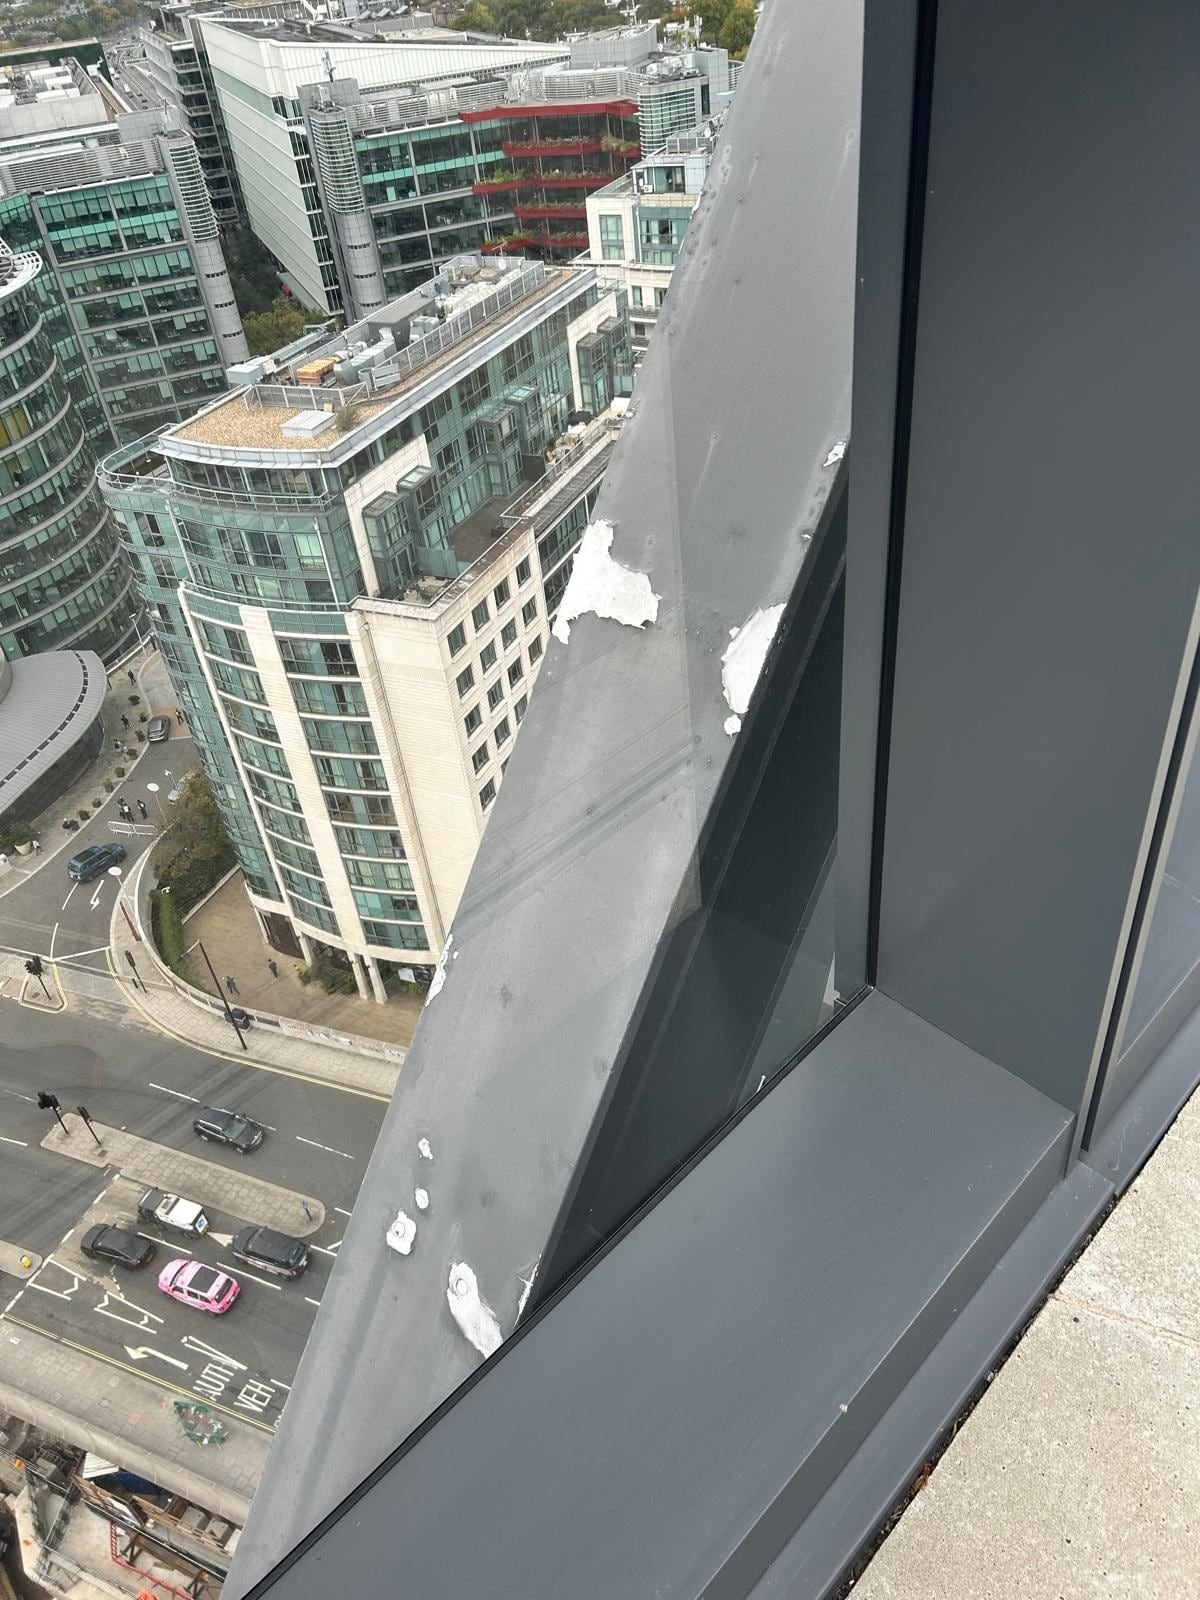
Root-cause analysis of coating defects, with clear evidence and corrective actions.
Find out more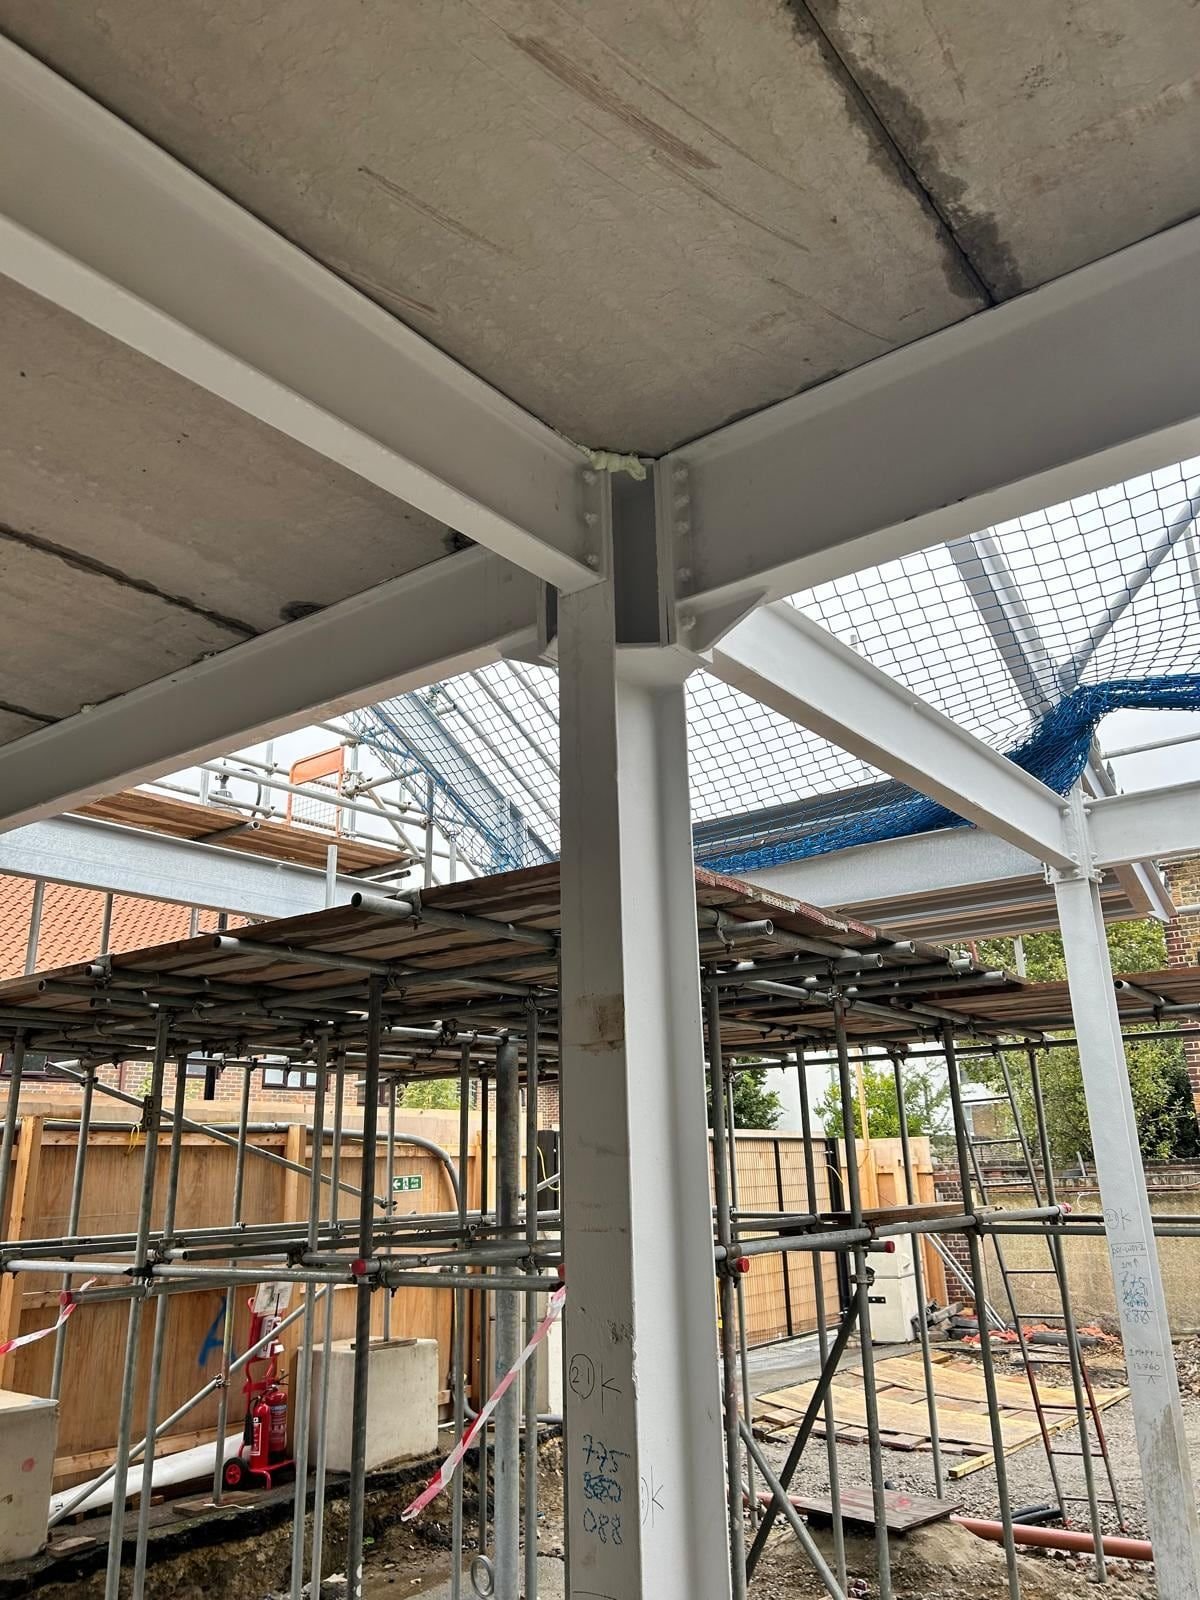
One point of contact for coating packages, from specification to handover.
Find out more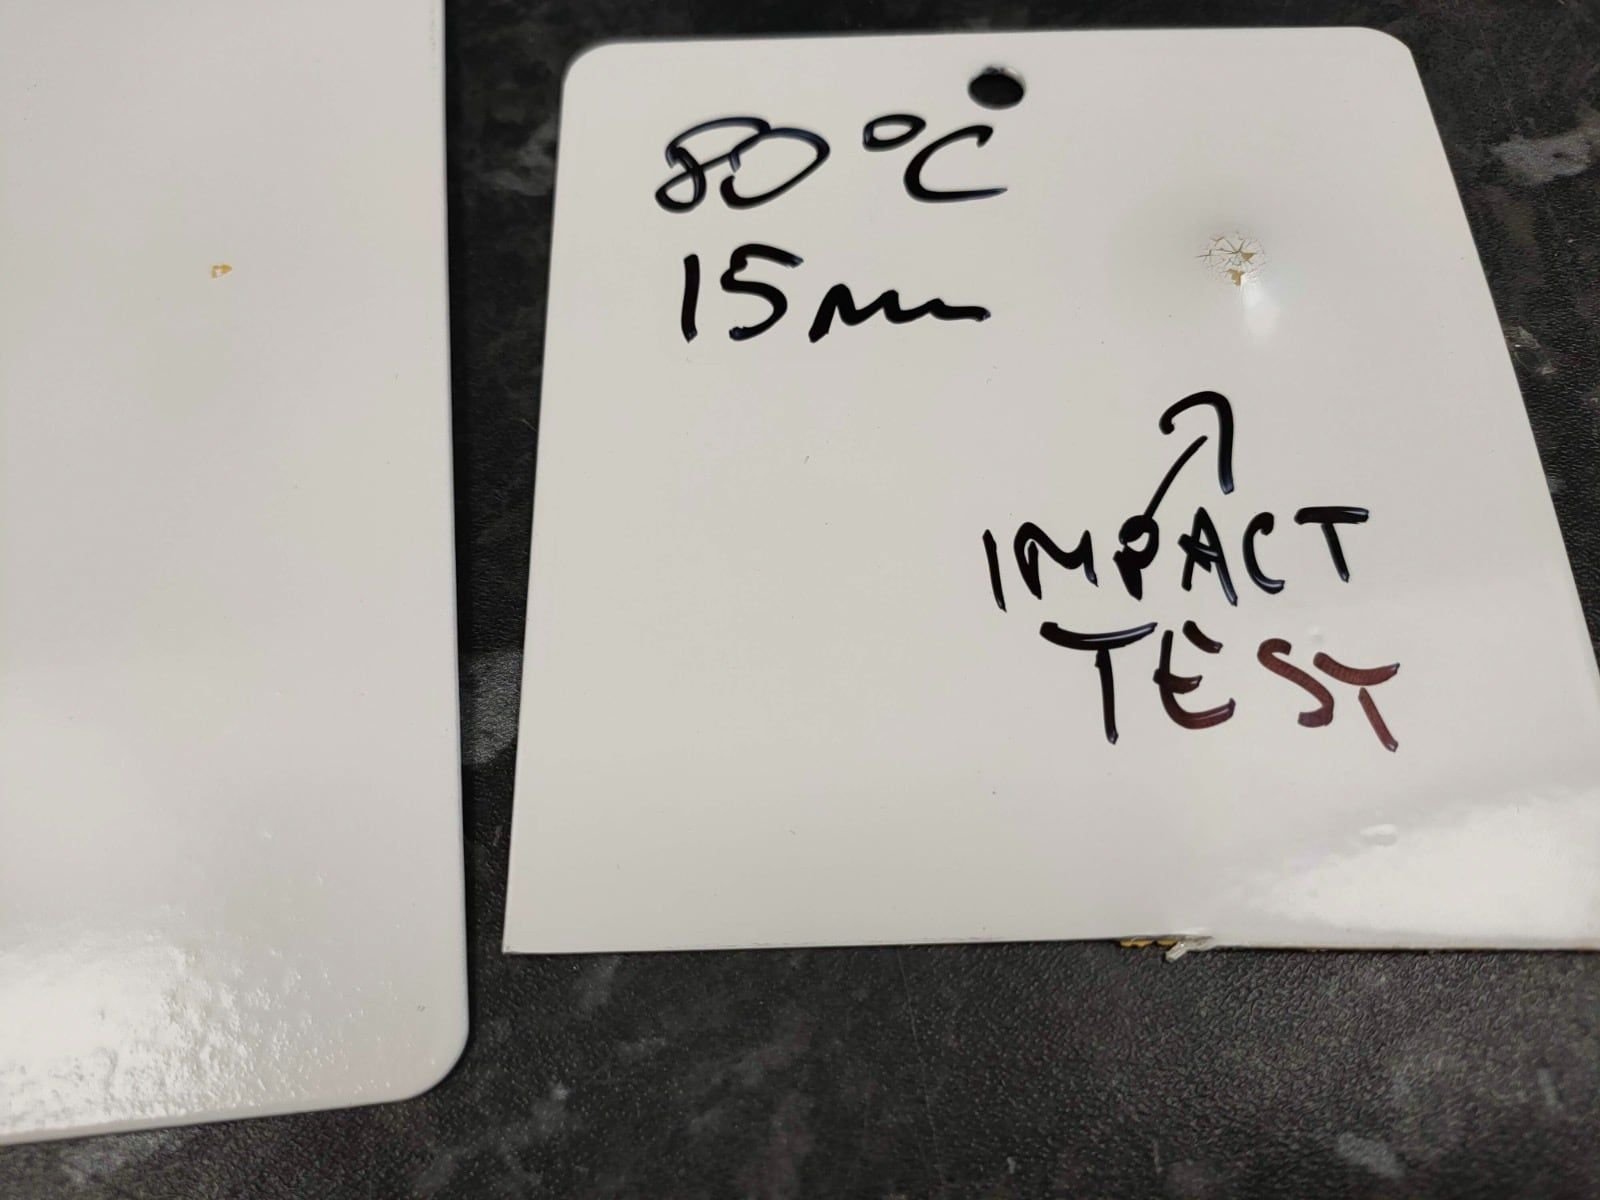
Documented, repeatable finishing processes, from R&D trials to production SOPs.
Find out more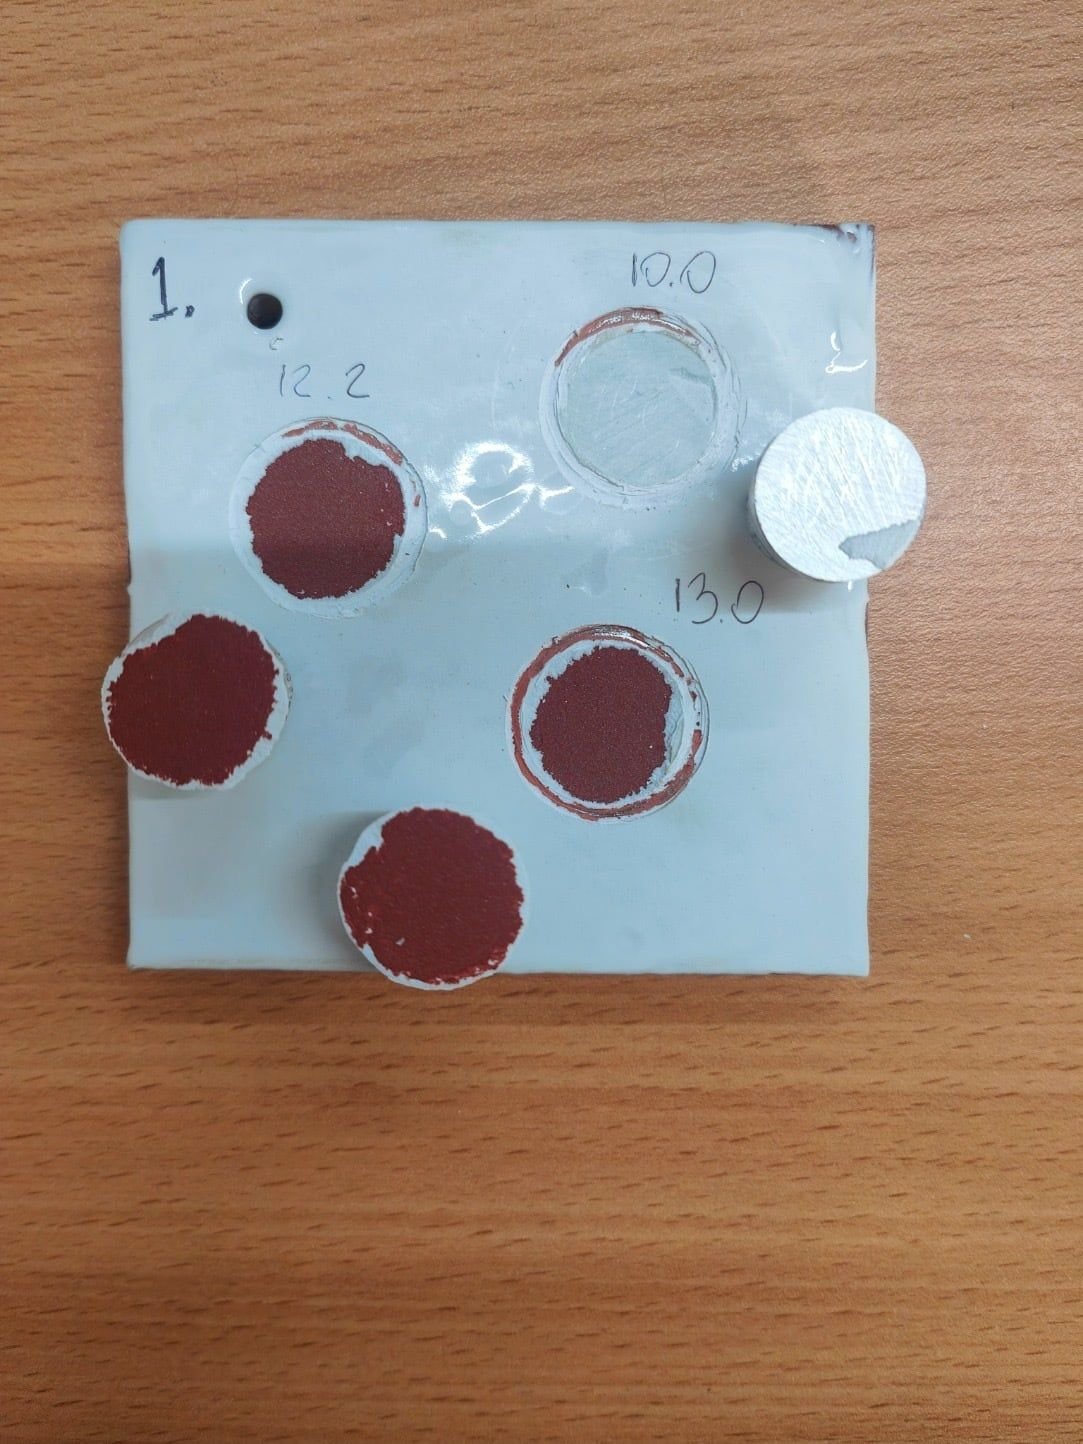
Get ready for ISO 9001, Qualicoat, Qualisteelcoat and coating-manufacturer audits.
Find out more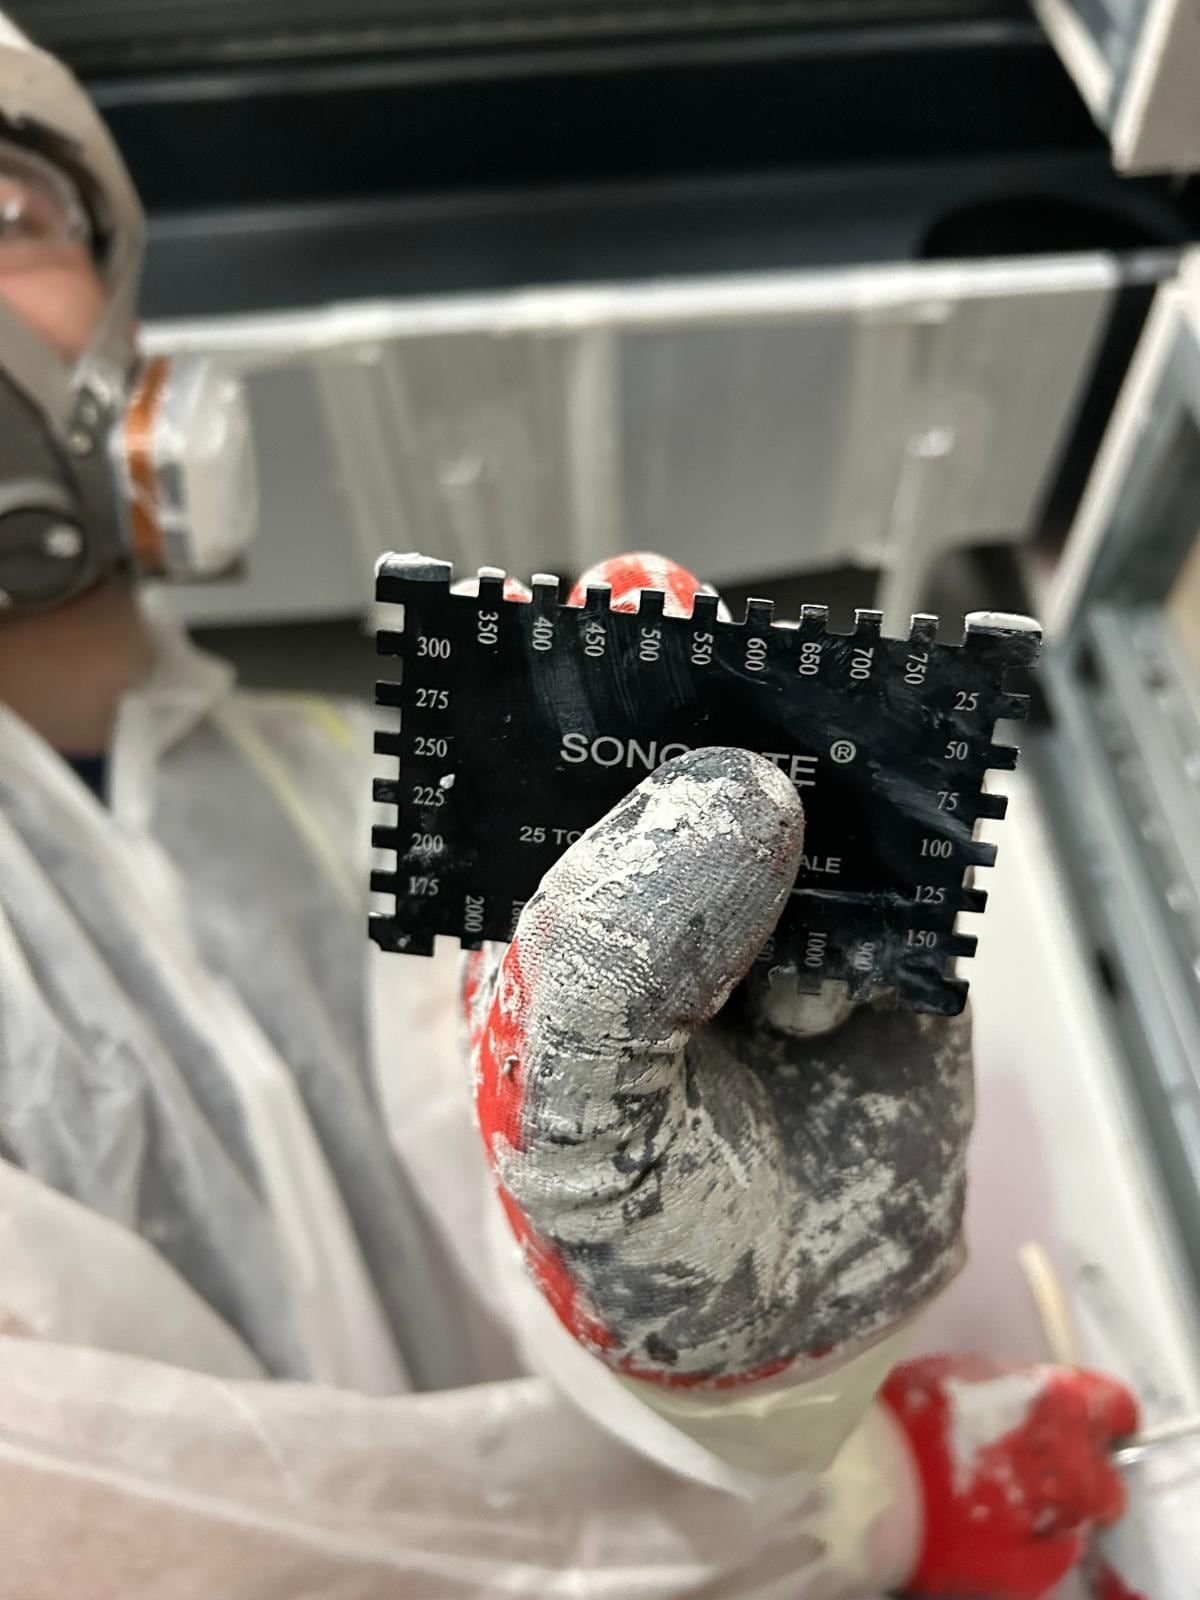
Technical training for the coatings industry, delivered at your premises in English, Polish or Slovak.
Training optionsHow a coating system is built
A typical three-coat protective system for a C4 environment. Once a coat is on, the one beneath it can never be checked again, so each stage has its own hold point.
Steel blast cleaned to Sa 2½ with a medium profile, free of dust and soluble salts.
Hold point: Grade, profile, dust and salts checked before priming.
Applied only when the steel is at least 3 °C above the dew point, inside the overcoating window.
Hold point: Climate logged, primer film thickness measured.
The barrier coat builds most of the thickness, with stripe coats on edges, welds and bolts.
Hold point: Edge and weld coverage, cumulative film build.
Colour, gloss and UV resistance, and the finish your client actually sees.
Hold point: Total DFT, adhesion where specified, final visual.
How we work
The same disciplined sequence on every job, whether it is one fabrication package or a full project.
We review the specification, data sheets and programme, and agree hold points before work starts.
Surface preparation inspected: steel condition, cleanliness grade, profile, dust and soluble salts.
Climate monitored against the dew point, wet film checked and overcoating windows respected.
Dry film thickness, cure, adhesion and appearance measured against the acceptance criteria.
Clear, traceable records with readings, photographs and any non-conformances closed out.
A complete documentation pack your client can rely on for the life of the coating.
How we inspect
Recognised methods, calibrated equipment and readings anyone can check. These are photographs from our own inspections.
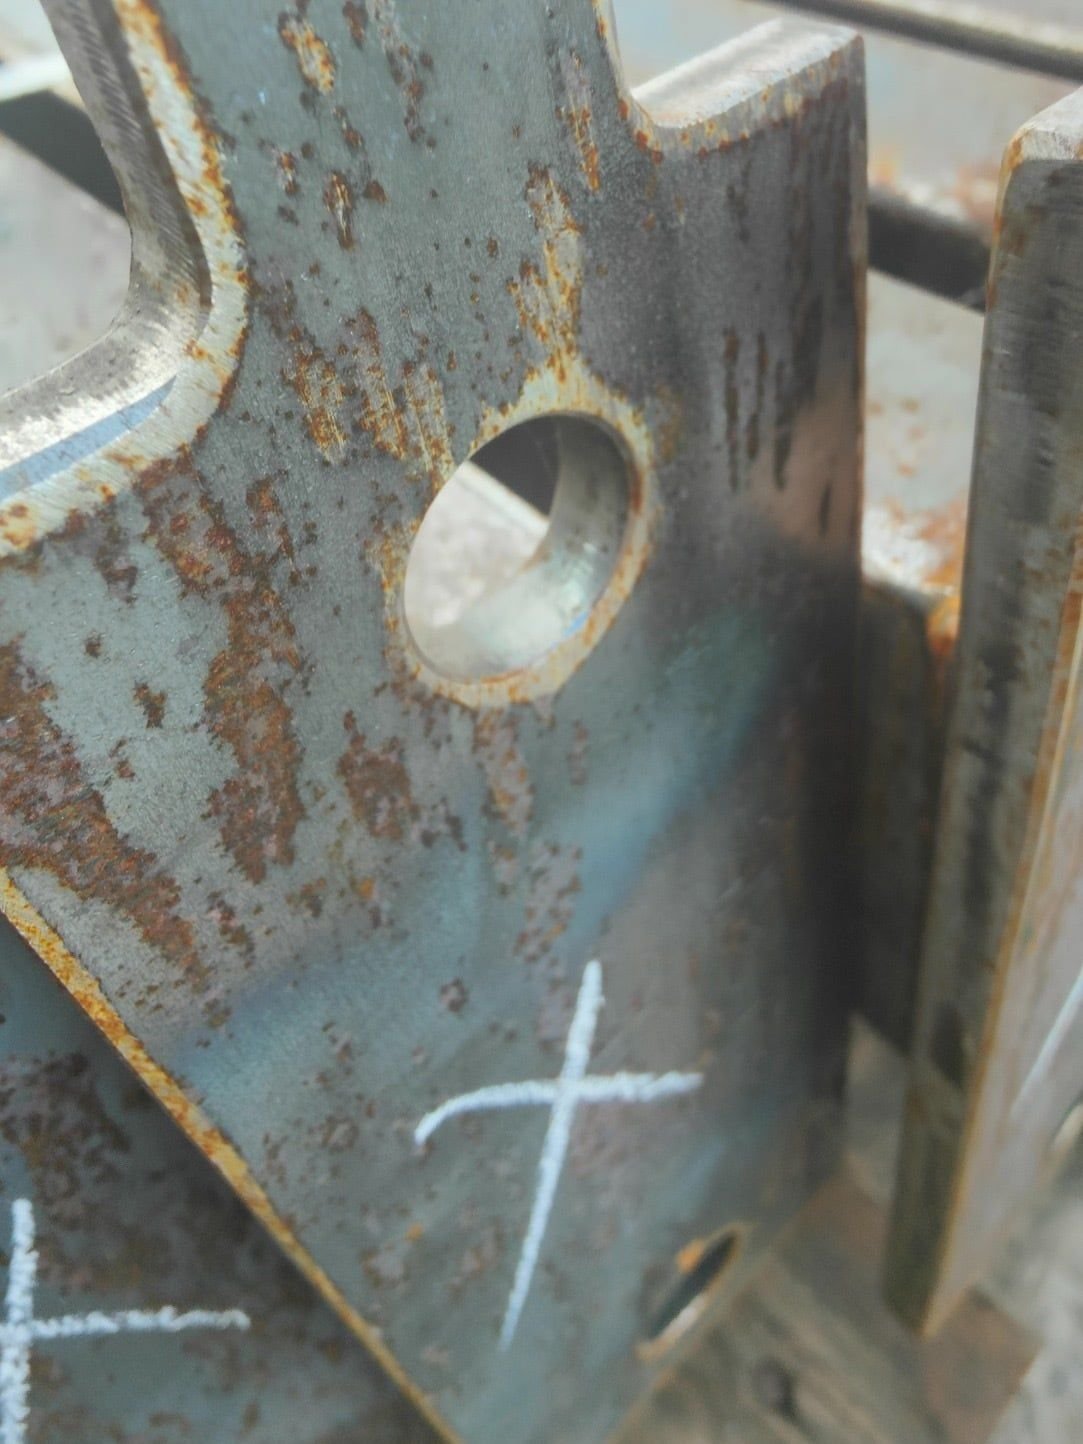
Steel assessed before surface preparation
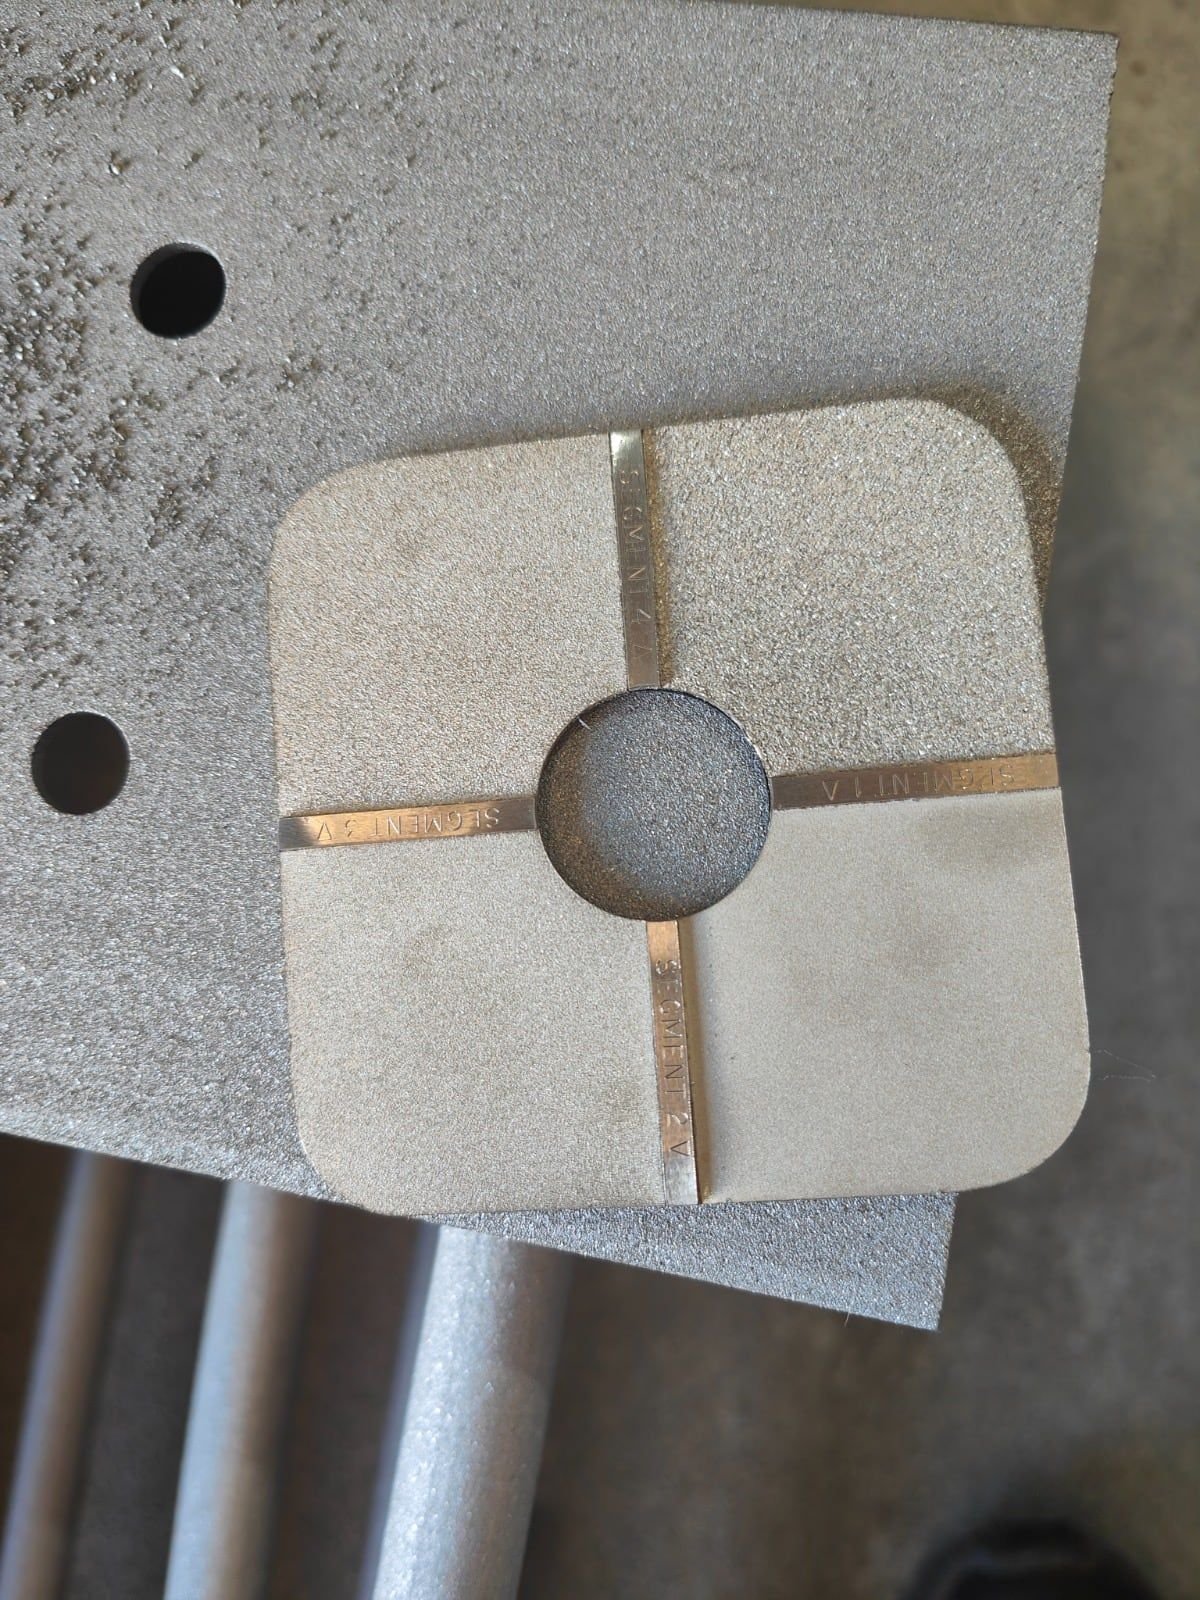
Blast profile checked against a comparator
Surface profile measured with replica tape
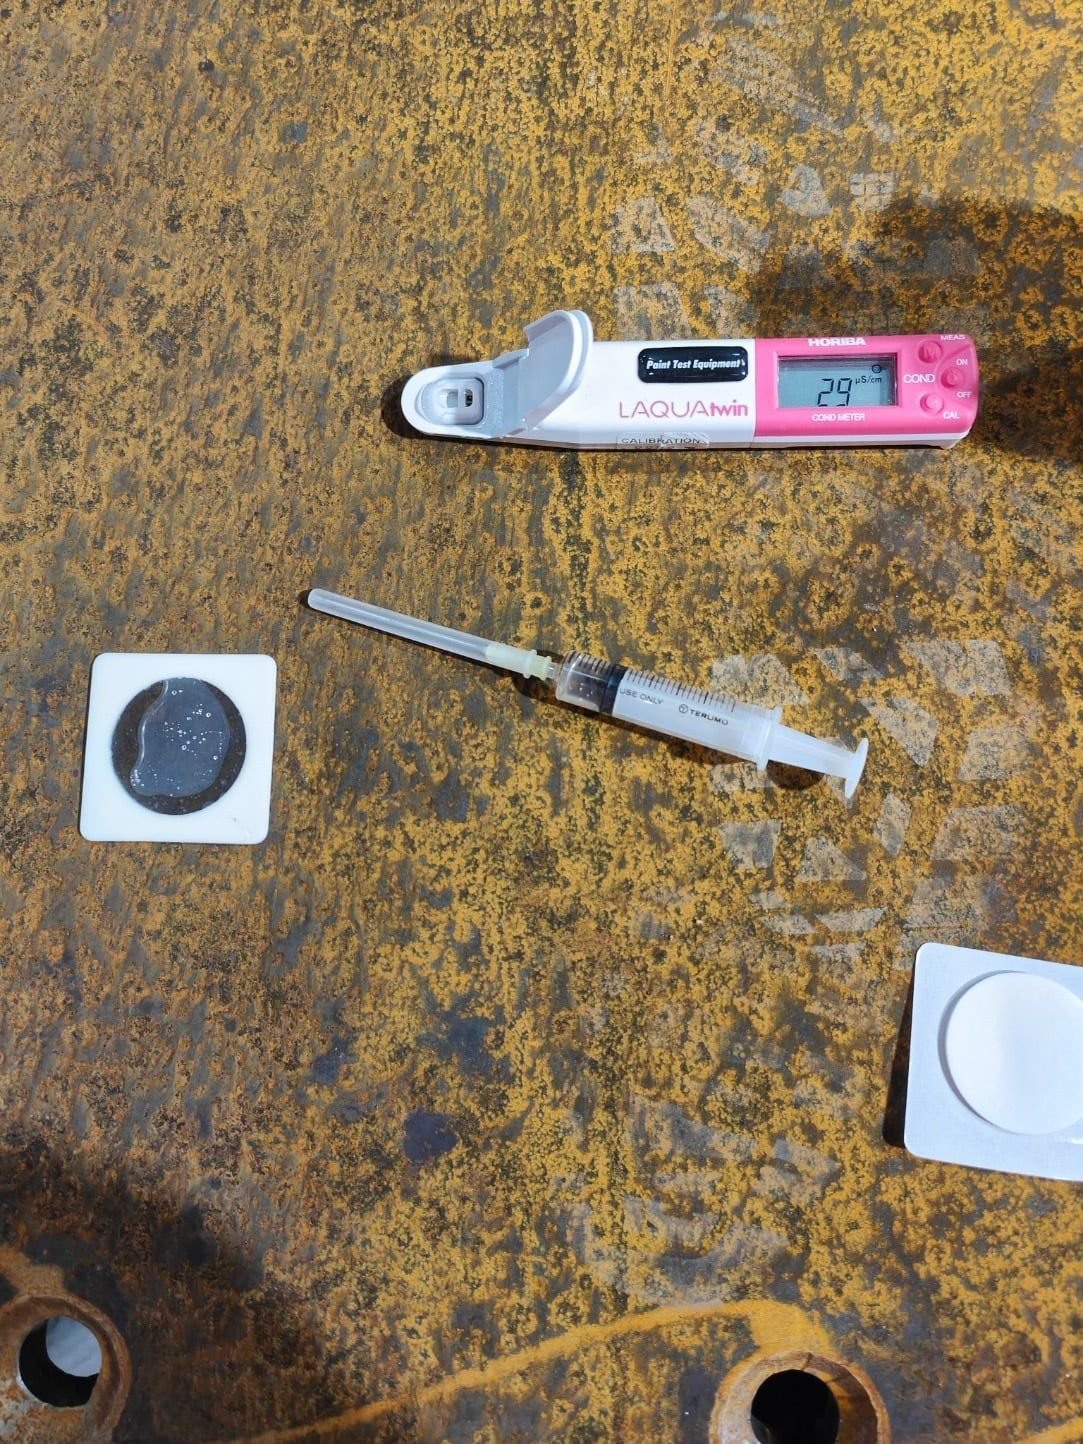
Soluble salt testing with a Bresle patch
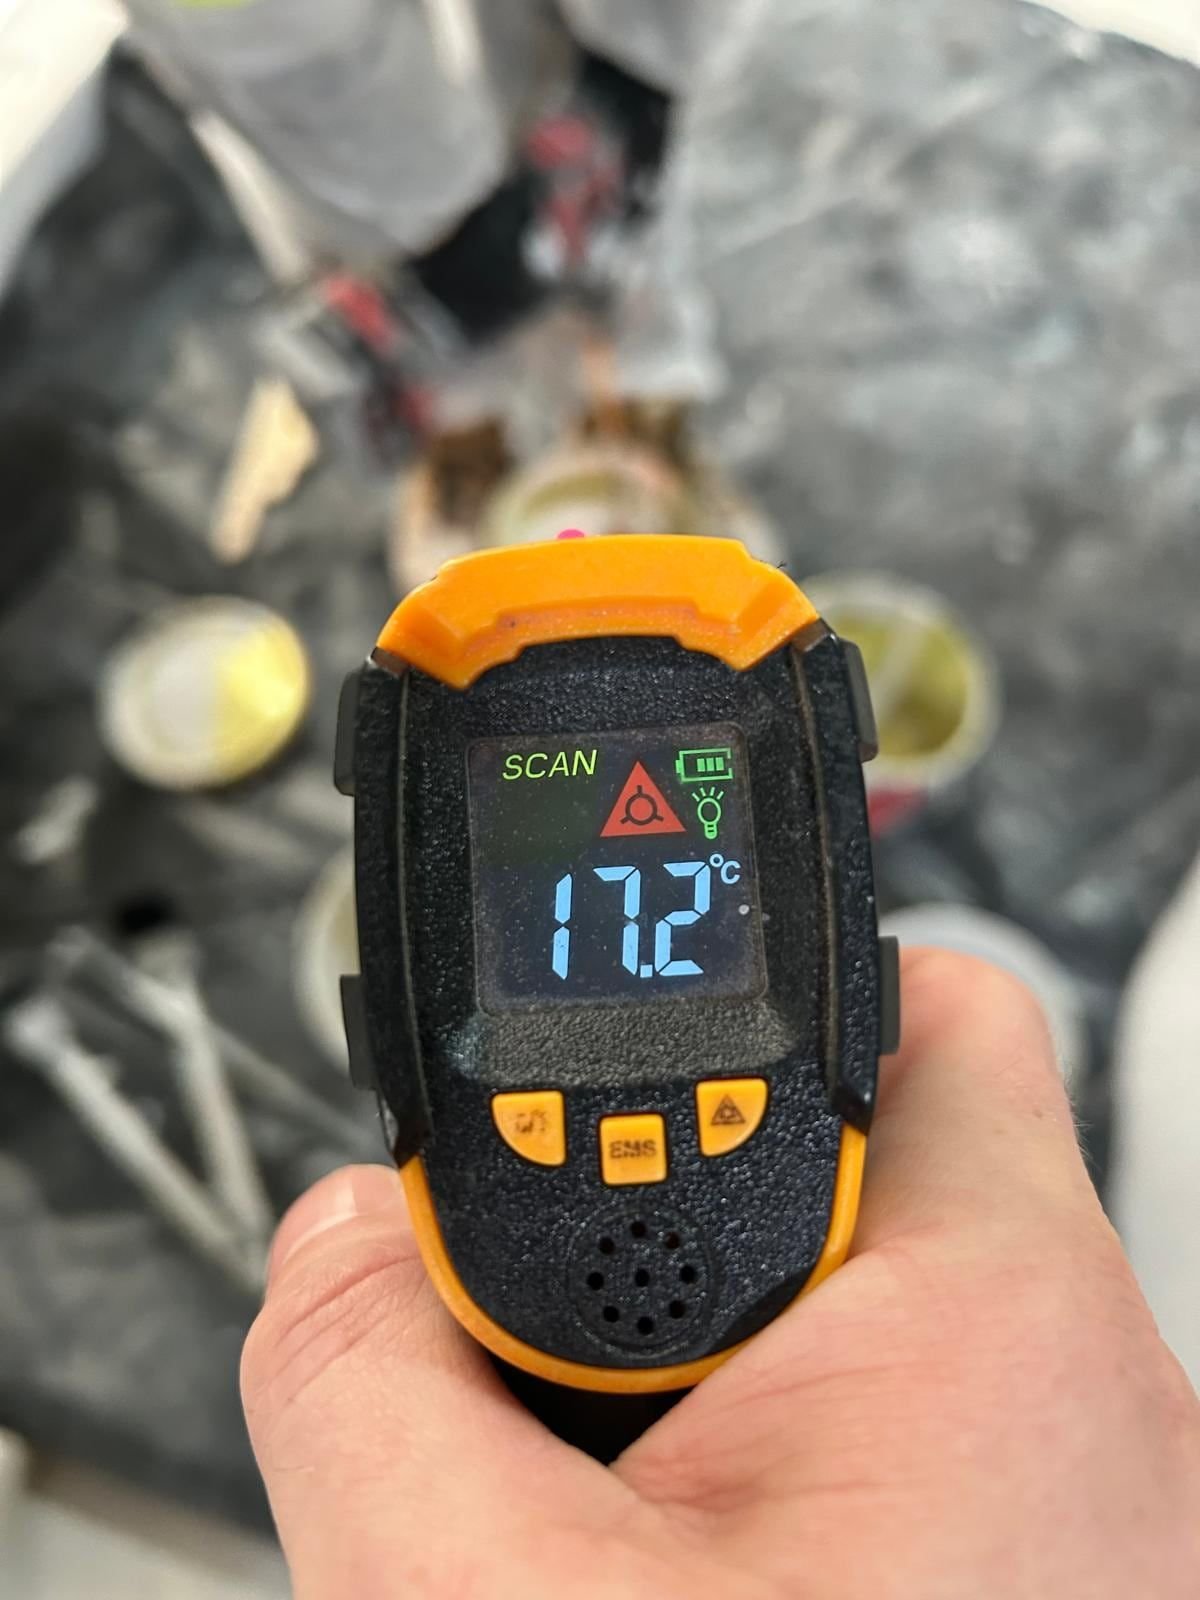
Surface temperature checked before coating
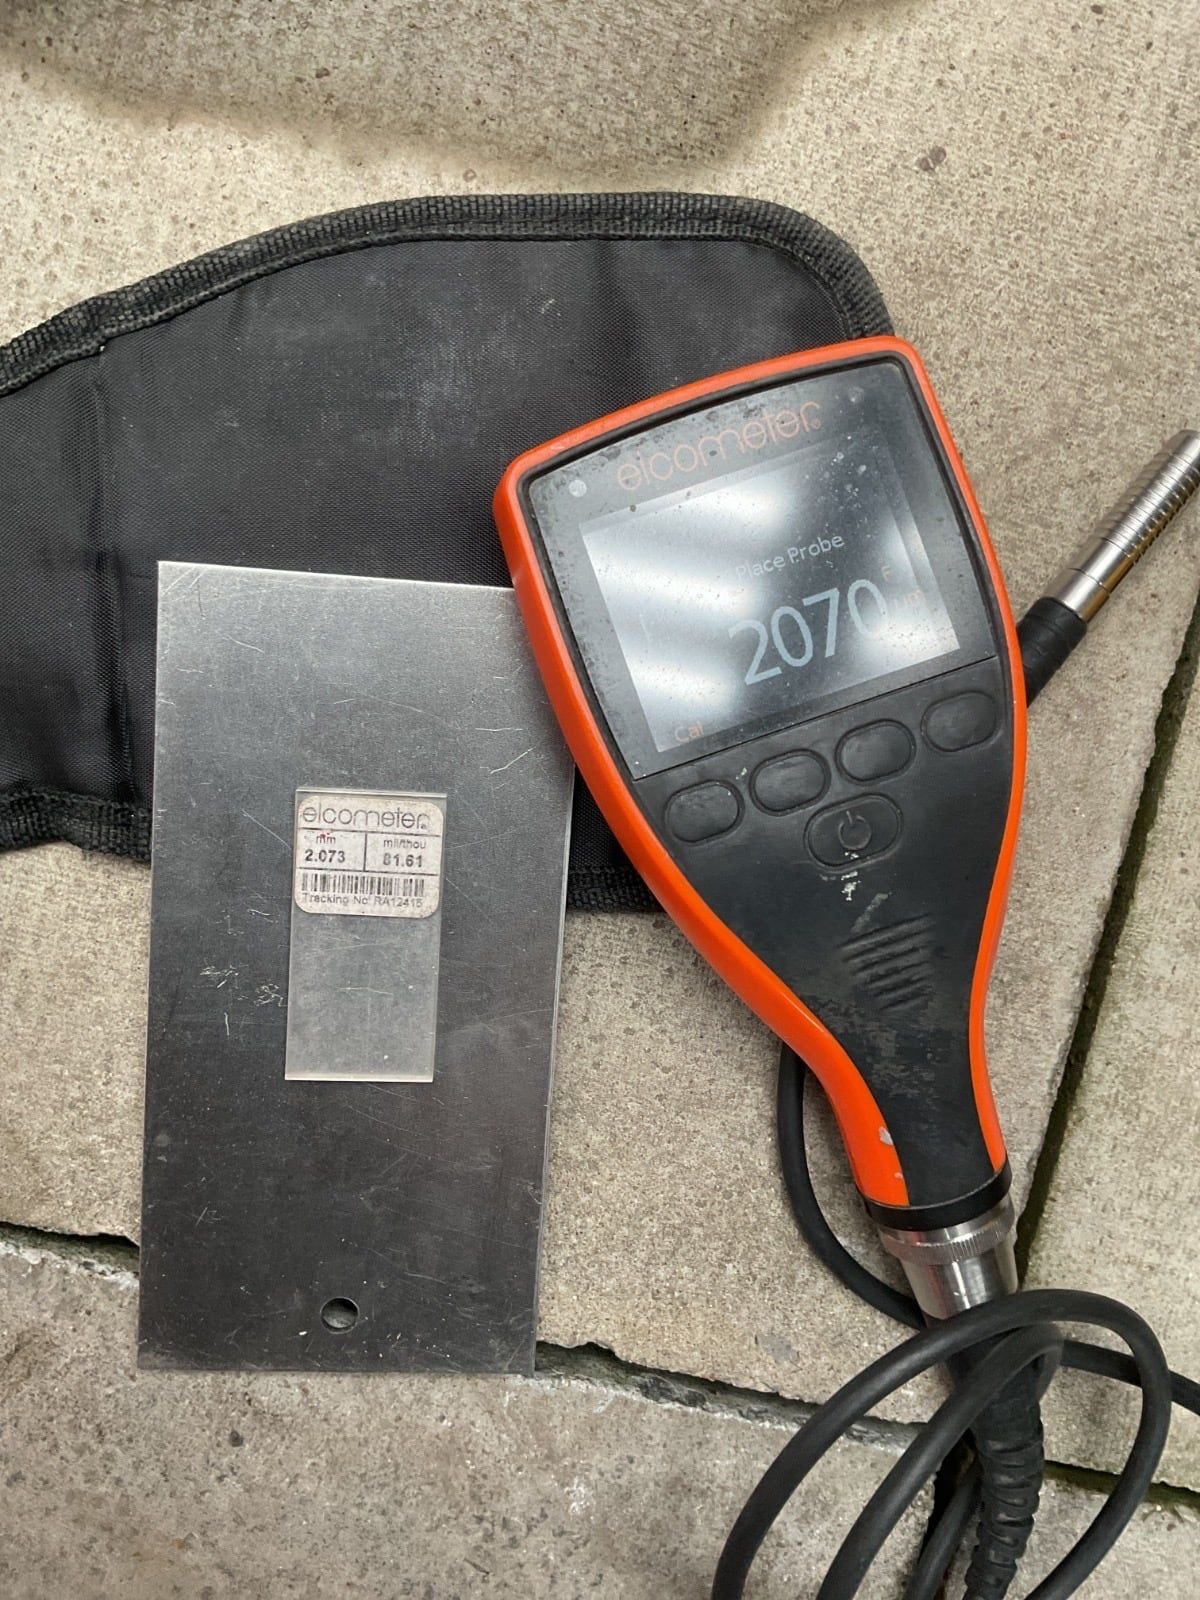
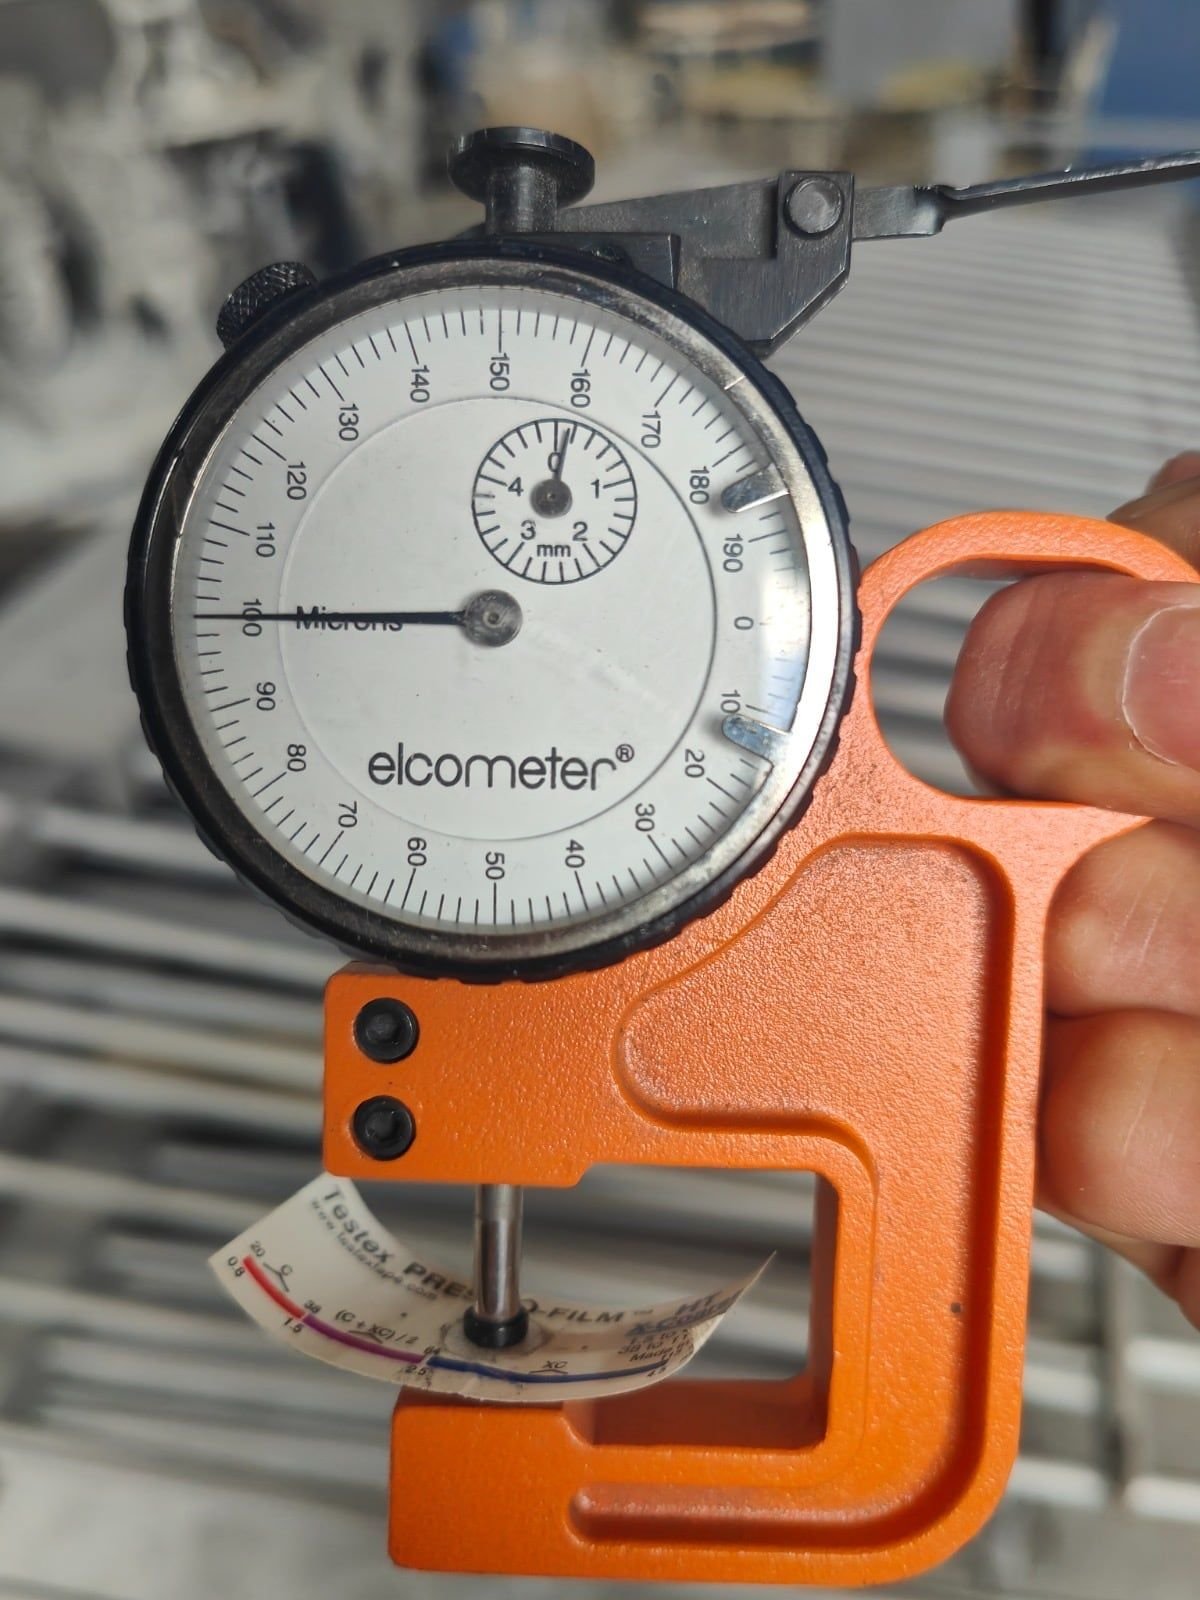
Gauge verified against a certified foil
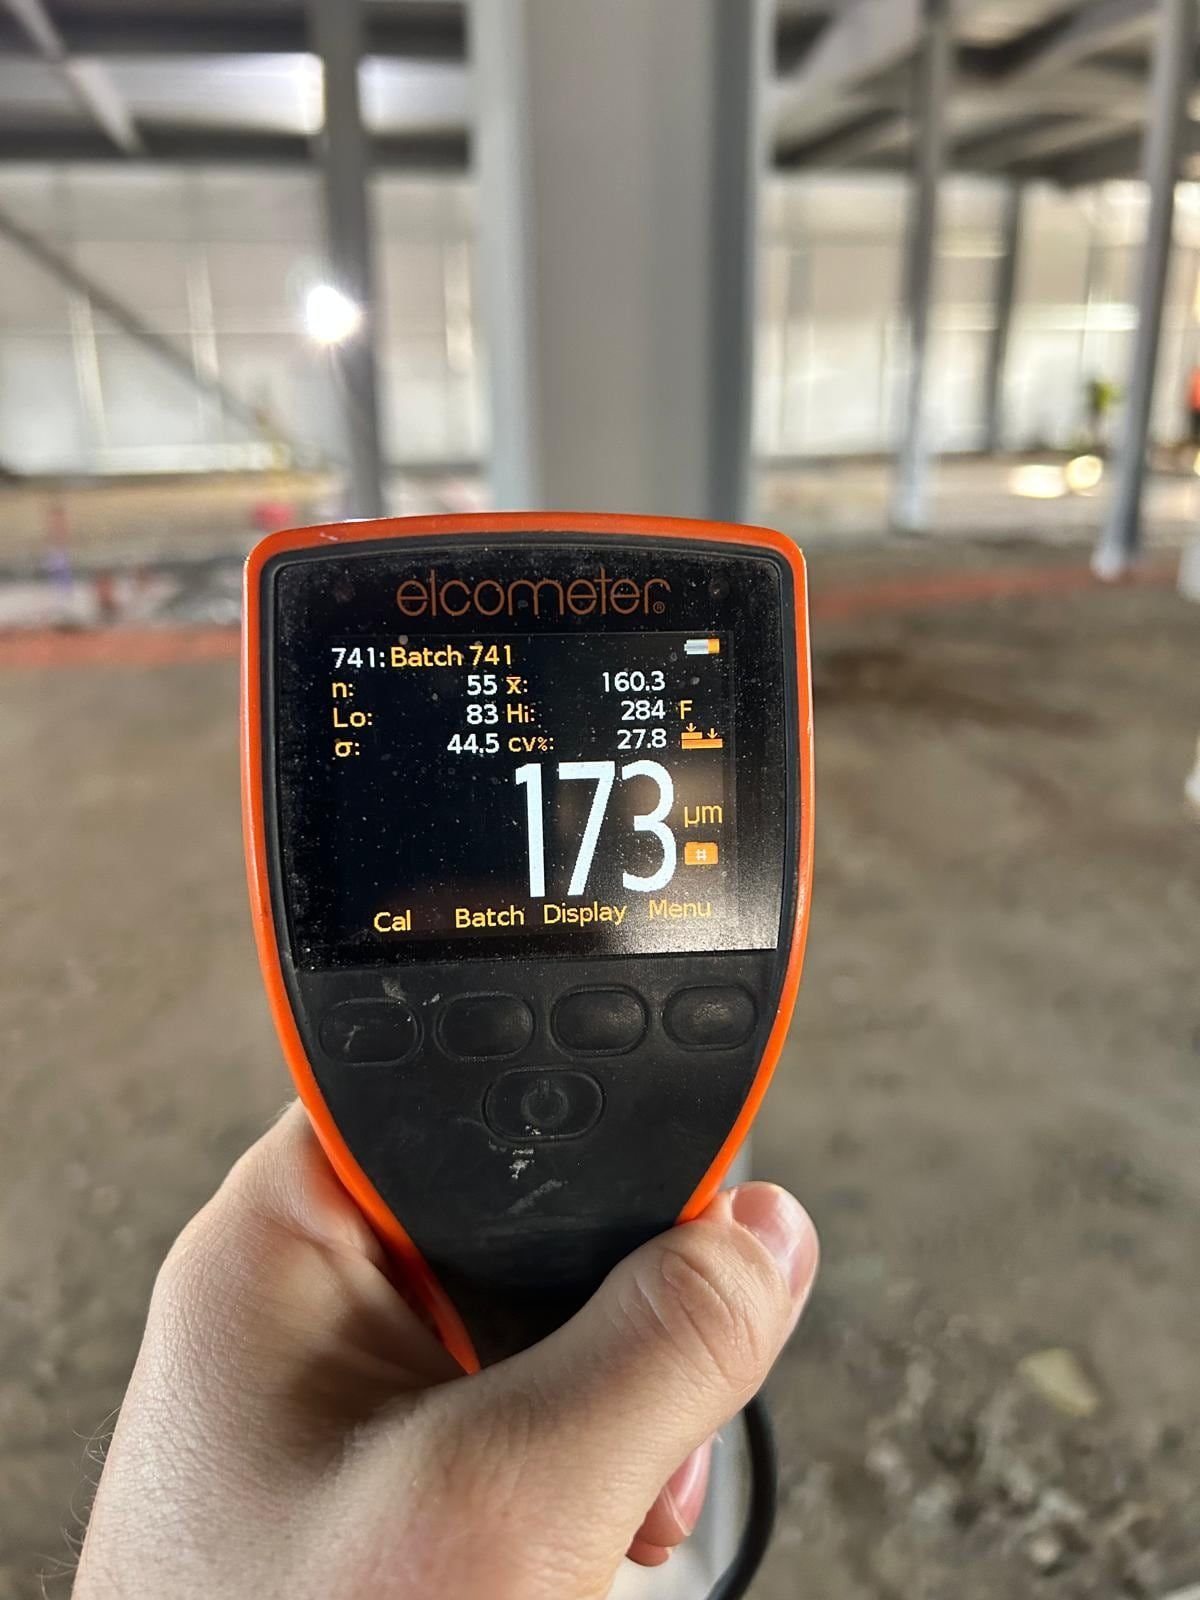
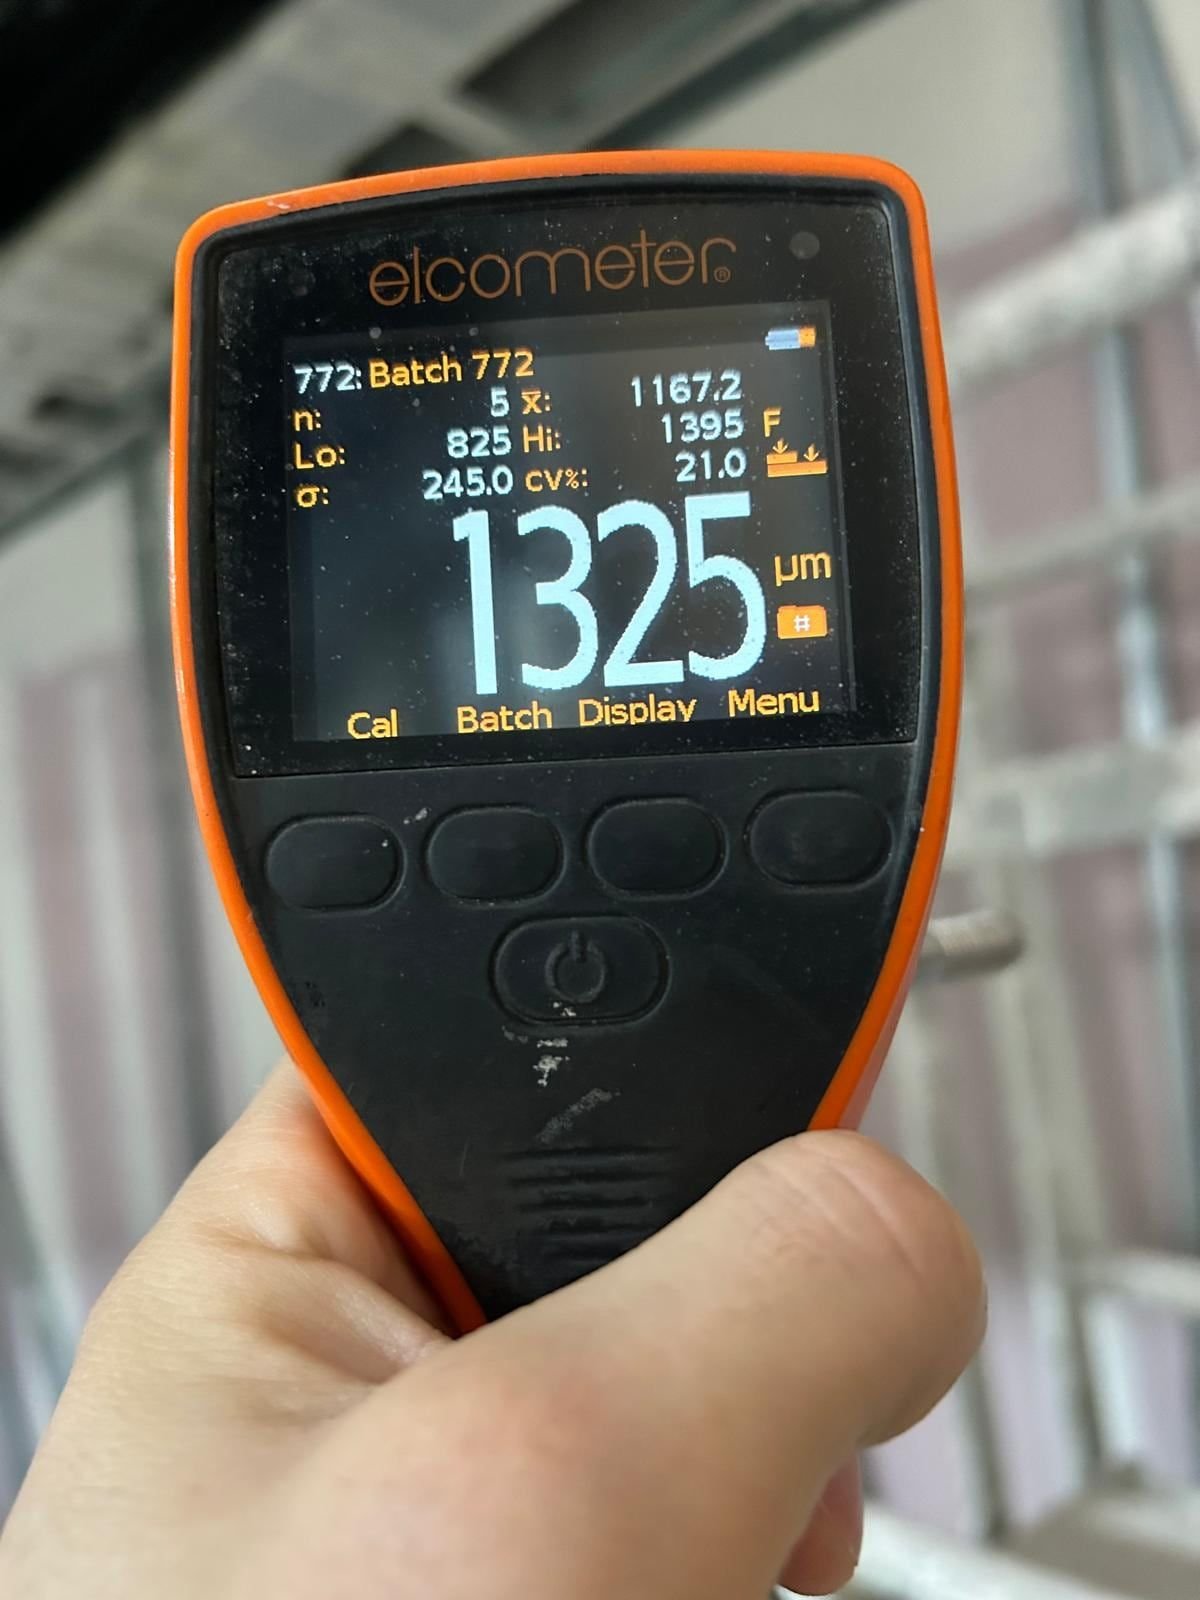
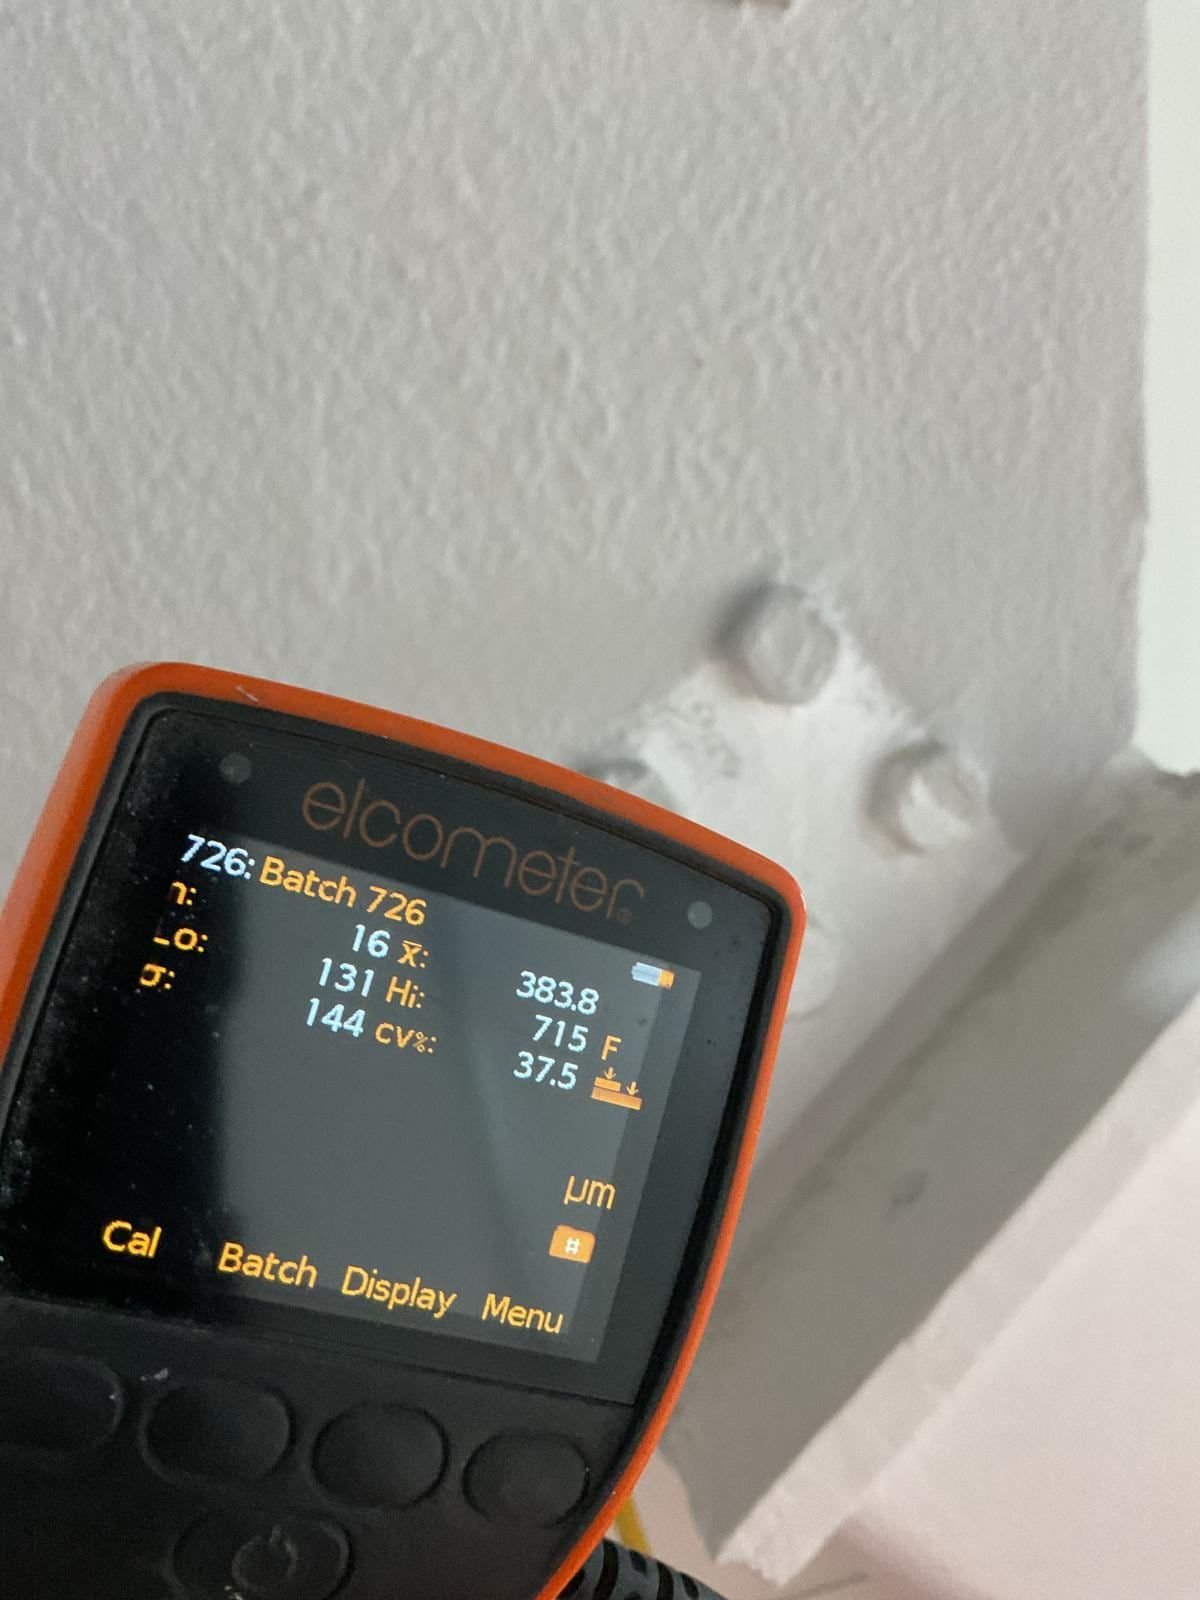
Dry film thickness, checked in microns
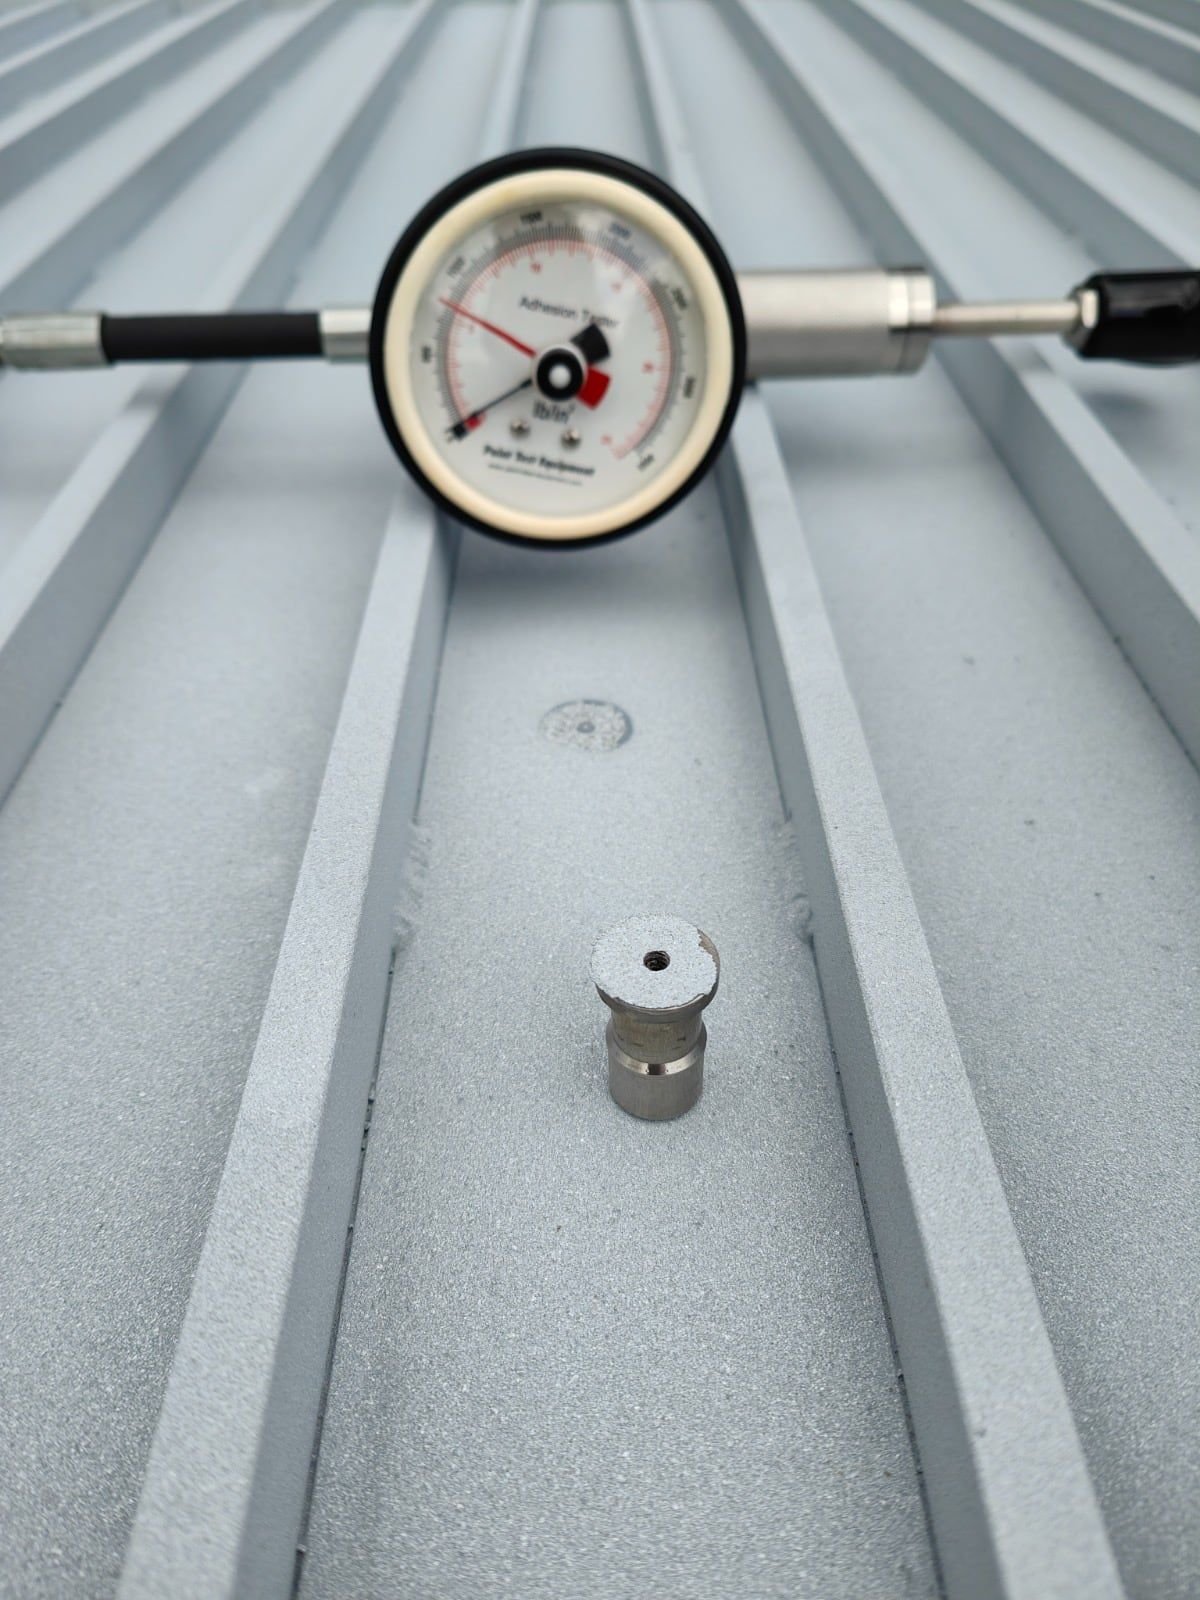
Pull-off adhesion tested on site
Industries
From data centres to nuclear: the same independent discipline, whatever the steel is for.
Not on the list? If it is metal and it needs a coating to last, we can almost certainly help. Ask us.
Why choose us
Independent, qualified and hands-on, on every project we support.
Independent and unbiased coating consultancy and inspection services
ICorr and AMPP coating inspection expertise
Expertise in chemical and mechanical surface preparation
Experience with powder coating and wet paint systems
Corrosion protection and coating performance expertise
Quality assurance and quality control support
Failure investigation and root-cause analysis
UK-wide project coverage
Experience supporting data centres, nuclear, infrastructure, manufacturing and architectural projects
Case studies
This work was carried out by our lead specialist before East Anglia Coating Solutions was established. The client and the previous employer are not named.
Failure investigation
Flaking and delamination on externally exposed structural steel, investigated so the project team could plan a repair from evidence rather than guesswork.
Pretreatment
A powder coating line asked whether its chemical pretreatment could meet the performance Qualicoat expects. The first panels failed. Adjusted dwell times put the next set right.
Coating inspection
An inspection of structural steel where primer thickness, access and surface preparation had been questioned, with a survey that separated compliant steel from steel that needed work.
Areas we cover
Our base is in Ipswich, with a strong presence throughout Suffolk, Norfolk, Essex and Cambridgeshire. For larger projects and inspection packages, we work throughout the UK.
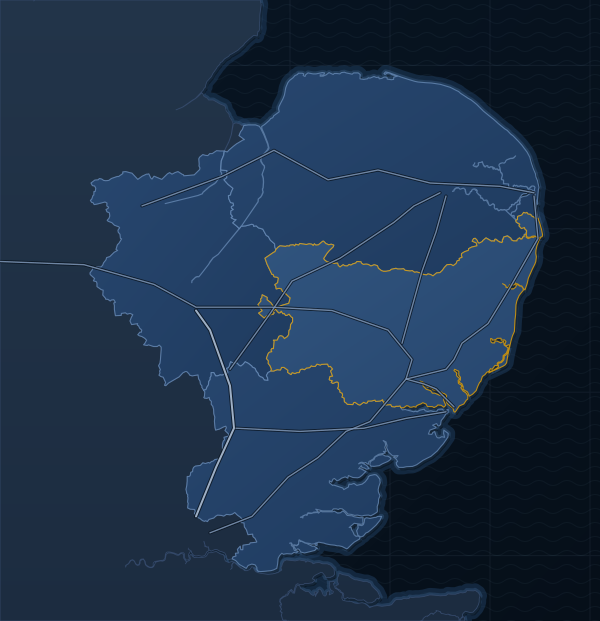
Boundaries: Office for National Statistics. Contains OS data © Crown copyright and database right. Roads approximate.
Resources
The questions we answer every week, written up properly: standards explained, defects diagnosed and a dew point calculator for site.
ISO 12944, ISO 8501 and more, in plain English.
OpenWhat each defect looks like, why it happens, how to prevent it.
OpenPractical articles on inspection, specification and quality.
OpenCheck steel temperature against the dew point on site.
OpenQuestions
If yours is not here, call us. We are happy to talk a problem through before you commit to anything.
Tell us about the job. We respond to all enquiries within one working day, with a clear scope and price.
Prefer to talk? Call 07810 022184